Best Heat Resistant Conveyor Belt Vendor from China for High-Temperature Conveying Solutions
2026-09-23
When conveyor belts start failing under extreme heat, production doesn't just slow down—it stops. That’s why finding the right heat-resistant conveyor belt matters more than most engineers realize. Among the many suppliers claiming to offer high-temperature solutions, XAN has built a reputation that’s hard to ignore. But what actually makes a conveyor belt truly heat resistant? And why are more operations turning to this Chinese vendor for answers? In this post, we’ll break down the key factors behind reliable high-temperature conveying—and what sets XAN apart from the usual options.
When Heat Resistance Claims Meet the Furnace Floor
Marketing brochures love the phrase “withstands extreme temperatures,” but the furnace floor has a way of interrogating such claims without mercy. A ceramic fiber blanket rated for 2300°F might survive a clean laboratory kiln, yet on a real furnace floor it faces thermal cycling, slag splash, and mechanical abrasion simultaneously. The result is rarely a dramatic failure—more often a slow, humiliating crumble that no datasheet ever predicted.
The gap between rated and actual performance widens further when you consider how heat resistance is measured. Standard tests use steady-state conditions: a small sample, a controlled atmosphere, a uniform heat source. But an industrial furnace floor is none of those things. Hot spots develop under burners, cold air sneaks in through charging doors, and molten metal occasionally drips onto surfaces that are supposed to be insulating, not sacrificial. This is where the phrase “heat resistant” quietly becomes “heat tolerant for a while.”
Savvy operators have learned to read between the lines of technical specifications. They look for third-party test reports, ask about thermal shock behavior, and—most tellingly—they visit a furnace that has been running for six months, not six hours. On that floor, the truth is written in cracks, spalled edges, and the faint smell of oxidized refractory. Claims that survive that inspection are the only ones worth paying for.
The Compound Tweaks That Separate Real Suppliers from Resellers
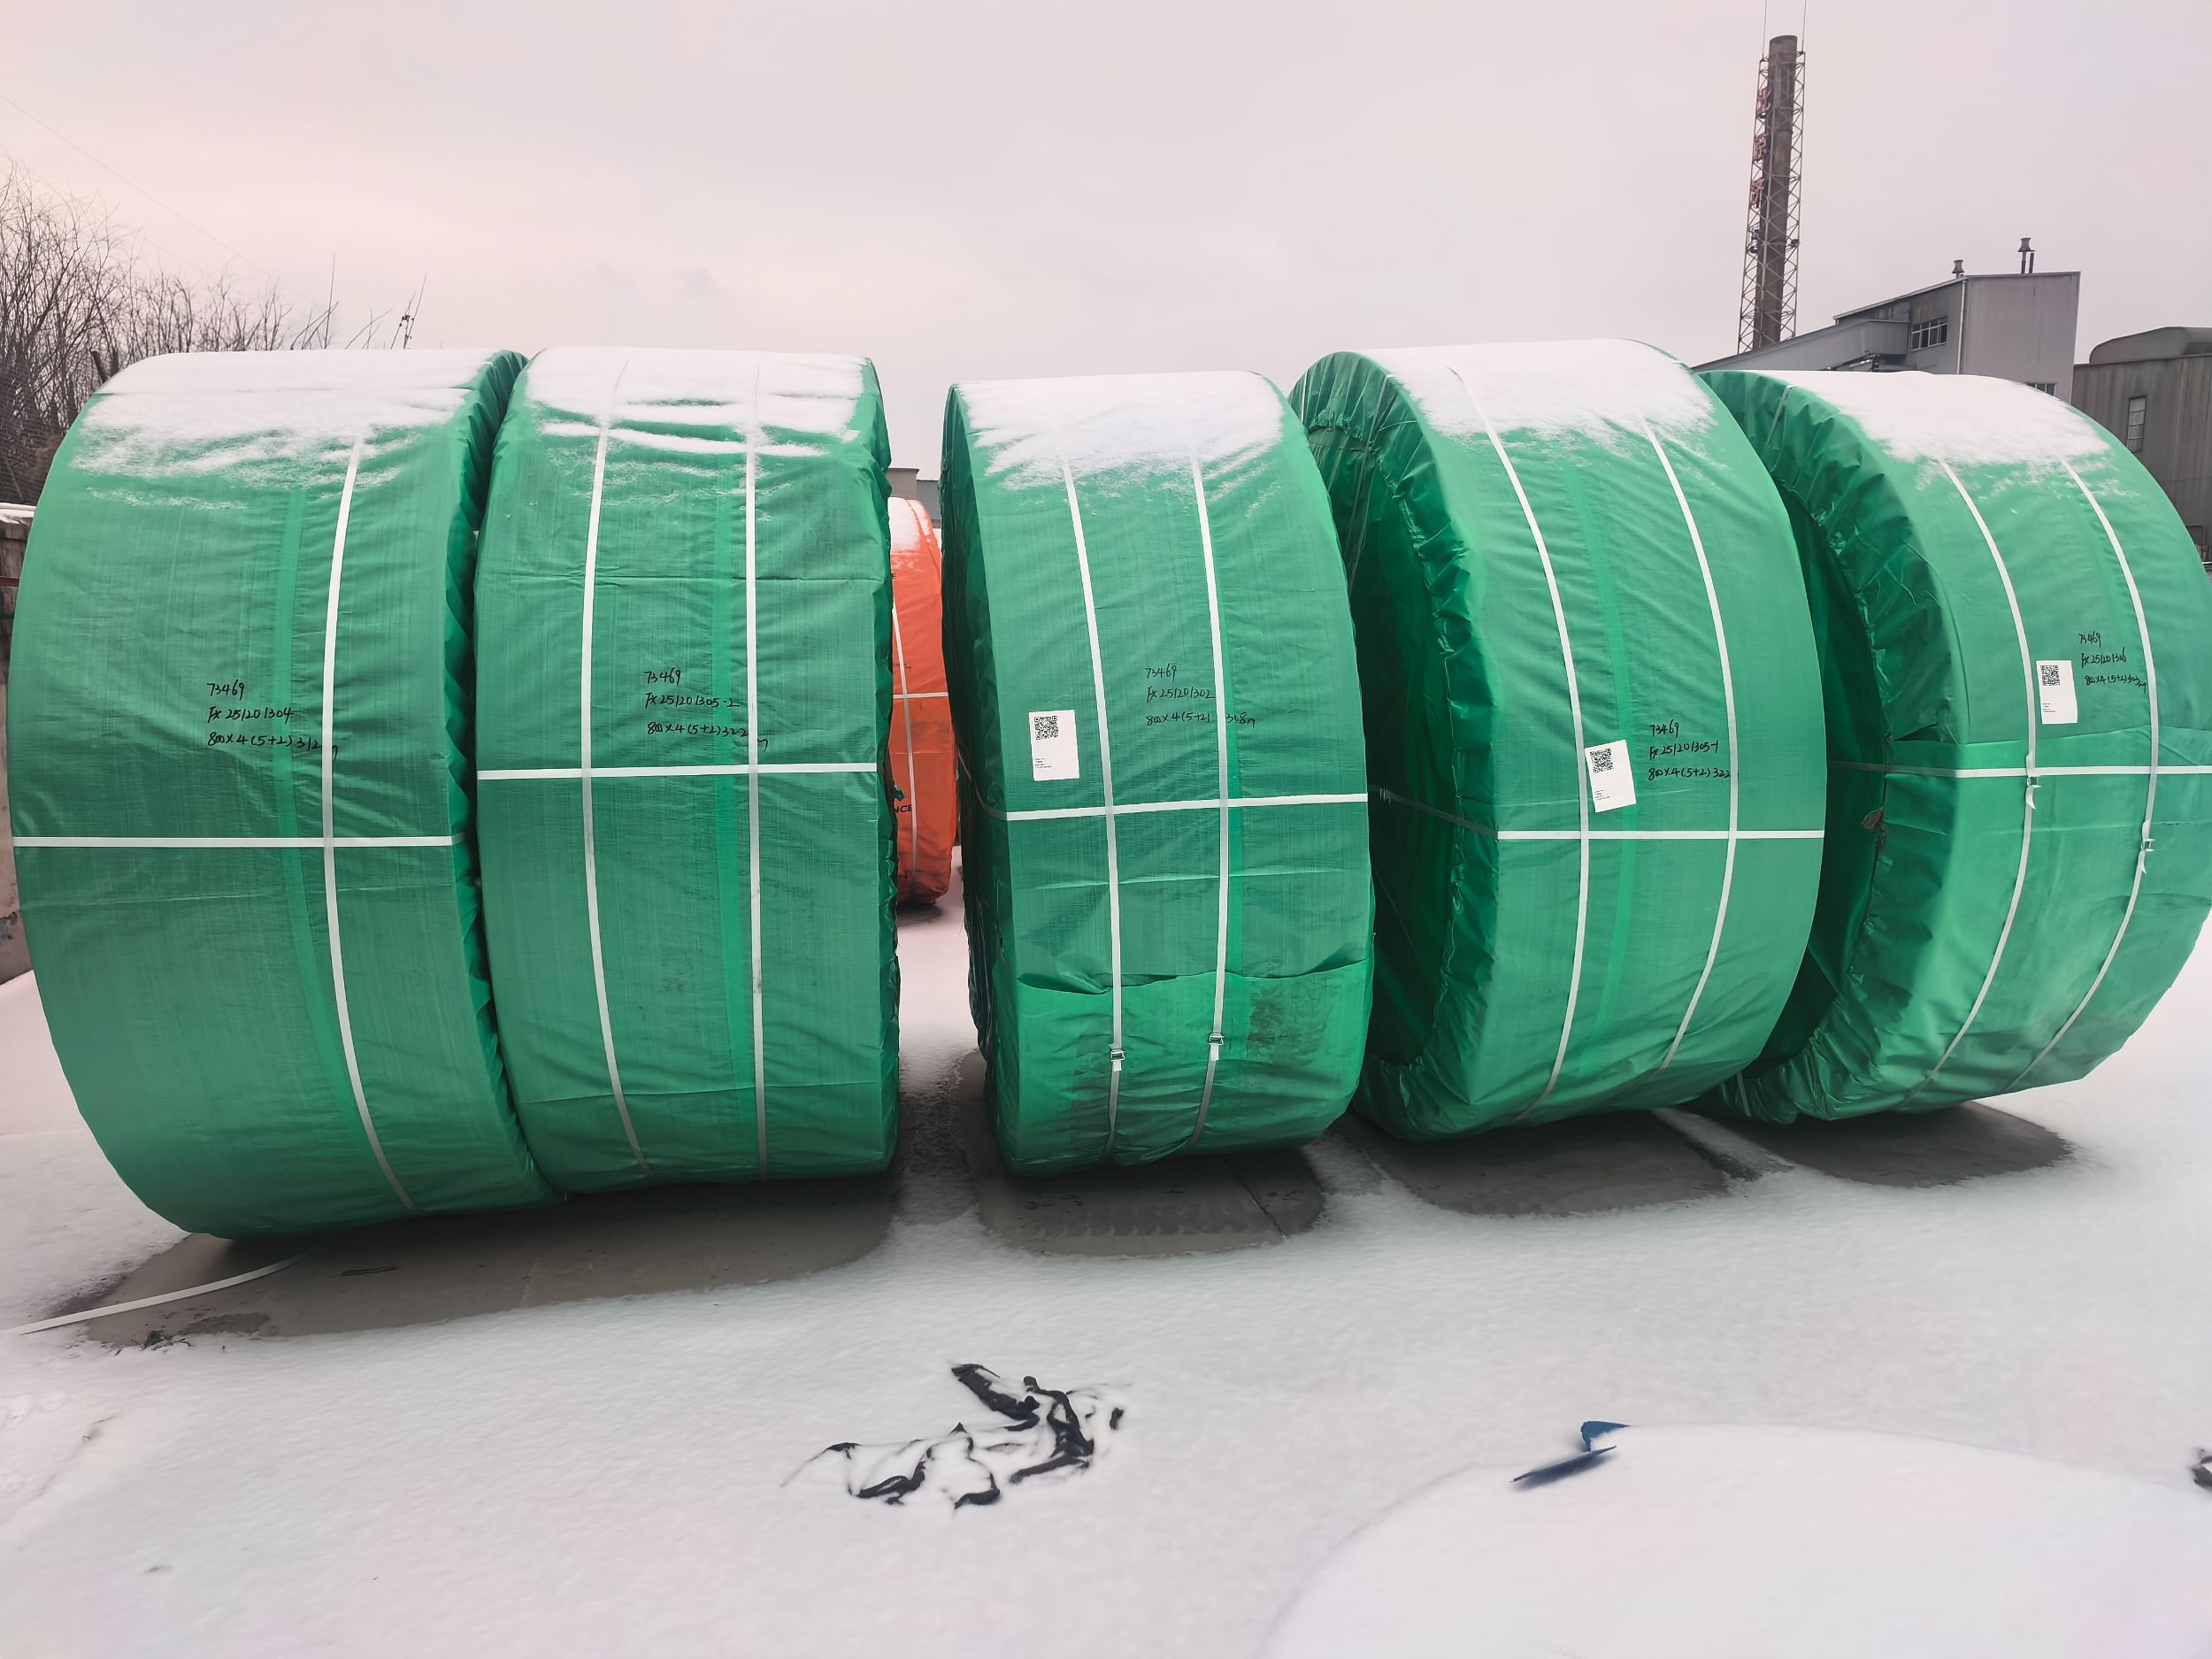
A genuine supplier rarely gets rattled when you ask to see the raw material batch sheets or the actual injection-molding parameters. They pull up a shared drive, walk you through the revision history on a part drawing, and tell you which line ran your sample at 2 a.m. because the humidity was lower. Resellers, on the other hand, start inventing reasons why the factory floor is off-limits or why the QC report is “confidential.” It is not one big red flag—it is the accumulation of small friction points: a vague answer about tolerances, a sudden change in the stated lead time, an invoice that lists a trading company’s address when the packing slip says something else. Those compound tweaks matter more than any single certificate.
Real suppliers also tweak their process around your order without making you beg. You ask for a slightly different durometer on a gasket and they come back with three test coupons and a note about the optimal cure time. You mention a packaging concern and they swap the carton divider layout, then send a video of the drop test. Resellers treat every change as a negotiation, because they are just relaying your request to somebody else and adding their margin. That delay, that loss of nuance, shows up in the final quote. A supplier who actually owns the line can absorb a compound adjustment in hours, not weeks—and they are not afraid to tell you when your “simple tweak” will actually weaken the part.
Eventually the difference shows up in small physical details: the mold gate location moved to reduce weld lines, the anti-rust paper switched to a thinner grade to avoid residue, the cable harness now has a slightly longer strain relief because the supplier noticed the bend radius on your CAD was questionable. Those are not flashy upgrades. They are the kind of things a reseller never sees, because a reseller never touches the part before it ships. Real suppliers accumulate tiny, unglamorous improvements over repeat orders, and that compounding is exactly what you are paying for—even when the unit price looks a few cents higher.
Inside the Test Rigs: Simulating 400°C Without Melting Down
Reaching 400°C in a lab isn't the hard part — keeping the rig itself from turning into a puddle is where the real engineering lives. The test chambers we use are lined with a sandwich of ceramic fiber and reflective stainless steel, but that's only the first line of defense. Every seam, bolt, and sensor port is a potential thermal leak, so we've had to re-think even the smallest components. Where a standard rig would use silicone gaskets, ours relies on compressed graphite and mica, materials that hold their shape long after conventional seals have given up.
Active cooling does the rest of the work. Instead of relying on passive insulation alone, we route a closed-loop coolant through channels machined into the outer shell — not water, but a high-flashpoint synthetic oil that won't vaporize under radiant heat. The trick is balancing flow rate against thermal expansion: too fast and you crack the ceramic core from thermal shock, too slow and the outer housing creeps past its rated temperature. We monitor the temperature delta across the shell in real time, adjusting the pump speed every few seconds rather than waiting for a full-feedback cycle.
What often gets overlooked is the instrumentation itself. Thermocouples rated for 400°C are common, but their sheaths and connectors are usually the first to fail. We've moved to bare-wire junctions inside ceramic tubes, with cold-junction compensation handled outside the hot zone. That way the sensor is reading the chamber, not its own melting connector. The result is a rig that can sit at 400°C for days without drifting, cracking, or quietly welding itself shut — which, trust me, happens more often than anyone likes to admit.
Lessons from Cement Kilns and Steel Mills That Run 24/7
Industrial operations that never sleep have developed a quiet mastery over chaos. Cement kilns and steel mills don't pause for weekends or holidays; they run hot and hungry, consuming raw material and energy in a continuous loop. The first lesson is about prediction before perfection. In these settings, downtime isn't an inconvenience—it's a cascade. A single stalled conveyor can back up raw feed, cool a kiln shell unevenly, and force a mill to run half-empty. So the operators learn to read subtle signals: a slight vibration in a bearing housing, a color shift in the flame, a change in the sound of grinding media. They don't wait for failure; they schedule interventions around the rhythm of the process itself.
Another hard-won insight is the value of walking the line between automation and human instinct. Modern plants are wired with sensors and predictive algorithms, but the best teams still rely on the person who has listened to the same motor for twenty years. That person knows when the data looks right but the machine sounds wrong. Cement and steel teach that reliability isn't built from dashboards alone—it's built from layered attention: digital alerts, yes, but also the gritty habit of physical inspection. A thermographer scanning a kiln shell isn't just collecting data; she's reading the story of the refractory brick underneath. These industries remind us that continuous operation is not about eliminating variability but about managing it so tightly that the inevitable becomes routine.
Finally, there is a cultural lesson about long-term thinking. A blast furnace reline happens once every fifteen to twenty years; decisions made today about raw material quality or cooling water chemistry will echo for decades. That forces a different kind of accountability. You don't optimize for this quarter's output alone—you optimize for the integrity of the entire asset across its lifecycle. In a world that celebrates fast iteration and pivots, cement kilns and steel mills stand as monuments to a slower, more deliberate form of excellence. Their lesson is clear: when you run 24/7, there is no shortcut to knowing your process deeply, caring for your equipment personally, and planning as if the next shift depends on this one—because it always does.
What to Ask Before You Trust a High-Temperature Belt Spec
A spec sheet can show a continuous rating of 600°F, but that number means little until you pin down the testing conditions behind it. Ask whether the temperature figure was recorded under actual load, with the belt moving, or simply in a static oven soak. Belts that pass a no-load chamber test often creep, stretch, or lose seam strength once a product weight and drive tension are introduced at the same heat. Request the time-at-temperature curve, not just a peak value, and find out if the belt was cycled between ambient and hot zones or held steadily at one point.
Next, drill into the failure modes that don't show up in a basic datasheet. A high-temperature belt may survive the heat while its coating embrittles, its edge reinforcement delaminates, or its tracking sleeve oxidizes after repeated passes. Ask for evidence of seam integrity after 500 or 1,000 hours, and clarify whether the belt was tested with your type of product contact — sticky resins, abrasive powders, and hot oils all degrade a belt differently than a clean, dry surface. If the supplier cannot show data from a similar application, set up a short pilot run with a reduced batch before committing to a full line.
Finally, compare the belt's thermal expansion rate against your oven or press frame. A material that grows 2% in length at operating temperature can walk off its pulleys or buckle under its own tension, and no static spec will catch that. Ask about the recommended pre-stretching procedure, the expected break-in period, and whether the belt needs a different tracking sensor or release coating once it reaches steady state. The goal is not to find a belt that merely survives a temperature number, but one that stays dimensionally stable, seam-sound, and chemically compatible after the process has been running for weeks.
Maintenance Habits That Keep Hot Belts from Cracking Early
Most cracking on hot belts starts long before it becomes visible. A habit that pays off is checking belt surface temperature with an infrared gun at three fixed points after shutdown, not during operation. Log those numbers weekly. If one spot runs more than 15–20°F hotter than the others, the usual suspect is a misaligned pulley or a dragging bearing, not the belt compound itself. Fix that early and the belt stops flexing through a hot, stretched zone.
Keep the belt clean without being aggressive. Fine dust and process residue bake onto a hot belt and act like abrasive grit inside the ribs. Use a soft brass brush or low-pressure air while the belt is still warm, but never a wire wheel or scraper. After installing a new belt, recheck tension within the first 8–10 hours of run time. Heat cycling causes initial stretch, and a slightly loose hot belt flexes more at the base of each rib, which is exactly where early cracks appear.
Cool-down discipline matters more than most people think. Don't spray water or blast compressed air onto a hot belt to speed up a shutdown. Let it cool naturally before doing any tension or alignment work. And store spare belts away from direct heat, steam lines, or sunny windows. A spare that sits at 120°F in a storage rack is already aging before it ever gets installed.
FAQ
Our belts are built to manage continuous material temperatures up to 400°C and can tolerate brief spikes around 600°C. The exact limit depends on the belt grade you choose, so we usually ask about your peak and average load temperatures before recommending a specific model.
You'll find them in cement plants, steel mills, foundries, power stations, and chemical processing facilities. Any operation moving hot clinker, sintered ore, ash, or similar materials tends to rely on these belts daily.
The covers typically use EPDM or SBR rubber compounds with added heat stabilizers, while the carcass may include high-strength polyester or aramid fabric. For extreme conditions, we also apply a glass fiber or aluminum foil layer to reflect radiant heat.
Yes, we manufacture to your exact specifications. Just send the belt width, length, pulley diameter, and trough angle, and we'll produce a belt that fits without field modification.
Every batch undergoes a thermal aging test and a tensile strength check before packing. We also use moisture-resistant wrapping and reinforced edge protection so the belts arrive in factory condition, even after long sea freight.
For standard heat resistant grades, expect about 15-20 days after deposit confirmation. Custom covers or non-standard widths may add another week. We always confirm a shipping date before you commit.
Absolutely. Each order includes a printed installation manual, and our engineers can walk your team through the first splice and tracking adjustment via video call if needed. We also suggest monthly checks on cover thickness in high-wear zones.
Yes, we split them into T1, T2, and T3 grades. T1 handles up to 100°C, T2 up to 200°C, and T3 up to 400°C continuous. This prevents overpaying for capability you don't need while keeping safety margins intact.
Conclusion
The gap between a supplier claiming heat resistance and a belt surviving on a furnace floor is where most procurement mistakes are made. When evaluating a Chinese vendor for high-temperature conveying, the first thing to check is whether they formulate their own rubber compounds or simply resell generic covers. Real manufacturers adjust the polymer blend, anti-oxidants, and carbon black dispersion to handle sustained exposure above 200°C, not just short peaks. Their test rigs matter too: a credible vendor runs a loop under constant tension inside a heated chamber that cycles between 250°C and 400°C, measuring elongation, hardness shift, and surface cracking for hundreds of hours. If the supplier cannot show you photos of their own test oven or share failure data from their lab, the spec sheet is probably borrowed from someone else.
Cement kilns and steel mills teach the harshest lessons because they run 24/7 with clinker and sinter at 300°C to 500°C. Belts that survive there have covers engineered for thermal oxidation resistance and a carcass that does not shrink or delaminate under continuous heat. Before trusting a high-temperature belt spec, ask how the vendor handles edge sealing, pulley lagging temperature limits, and the expected drop in tensile strength after three months at the rated temperature. A good Chinese supplier will give you a derating curve, not just a single number. Maintenance habits also separate long-lived belts from early failures: rotating the belt, keeping skirting pressure low, avoiding direct flame impingement, and monitoring for local hot spots prevent the classic transverse cracks at the edge. In the end, the best vendor is the one who treats your application like a test plan, not a sales ticket.
Contact Us
Contact Person: Anna Lu
Email: [email protected]
Tel/WhatsApp: 8618561668850
Website: https://www.x-conveyor.com