China Temporary Protective Film Manufacturer Selection Tips for Quality Assurance
2026-08-13
When you're importing temporary protective film from China, the difference between a seamless production run and a costly rework often comes down to one thing: manufacturer selection. With countless suppliers claiming top quality, how do you separate genuine capability from clever marketing? This guide breaks down practical quality assurance tips, drawing on insights from Shire—a name that has learned what truly matters on the factory floor.
Verify raw material traceability before committing to a supplier
Traceability isn't a box to tick after the contract is signed. It's the first real test of whether a supplier can back up their claims with paperwork, not promises. Ask for a clear map of where each raw material originates, how batches are labeled, and what happens when something goes wrong mid-stream. A supplier who hesitates to share this level of detail—or offers vague assurances instead of documentation—is telling you something important about how they'll handle surprises later.
Go beyond the certificate on the wall. Request actual lot-level records, shipping logs, and any third-party audits tied to the specific materials you'll be buying. A single certificate for a supplier's entire facility doesn't prove that your order's cotton came from the farm they claim, or that the metal in your components wasn't mixed with lower-grade stock. Real traceability means you can follow the chain backward from their warehouse to the source without gaps.
Make this verification a precondition, not a formality. If a supplier can't demonstrate end-to-end visibility before you commit, walk away. The cost of switching now is far lower than discovering six months into production that you've been sold materials with unknown origins, forced labor risks, or quality inconsistencies. Solid traceability isn't about perfection—it's about a supplier who treats your supply chain as seriously as you do.
Ask for real production line footage, not polished brochures
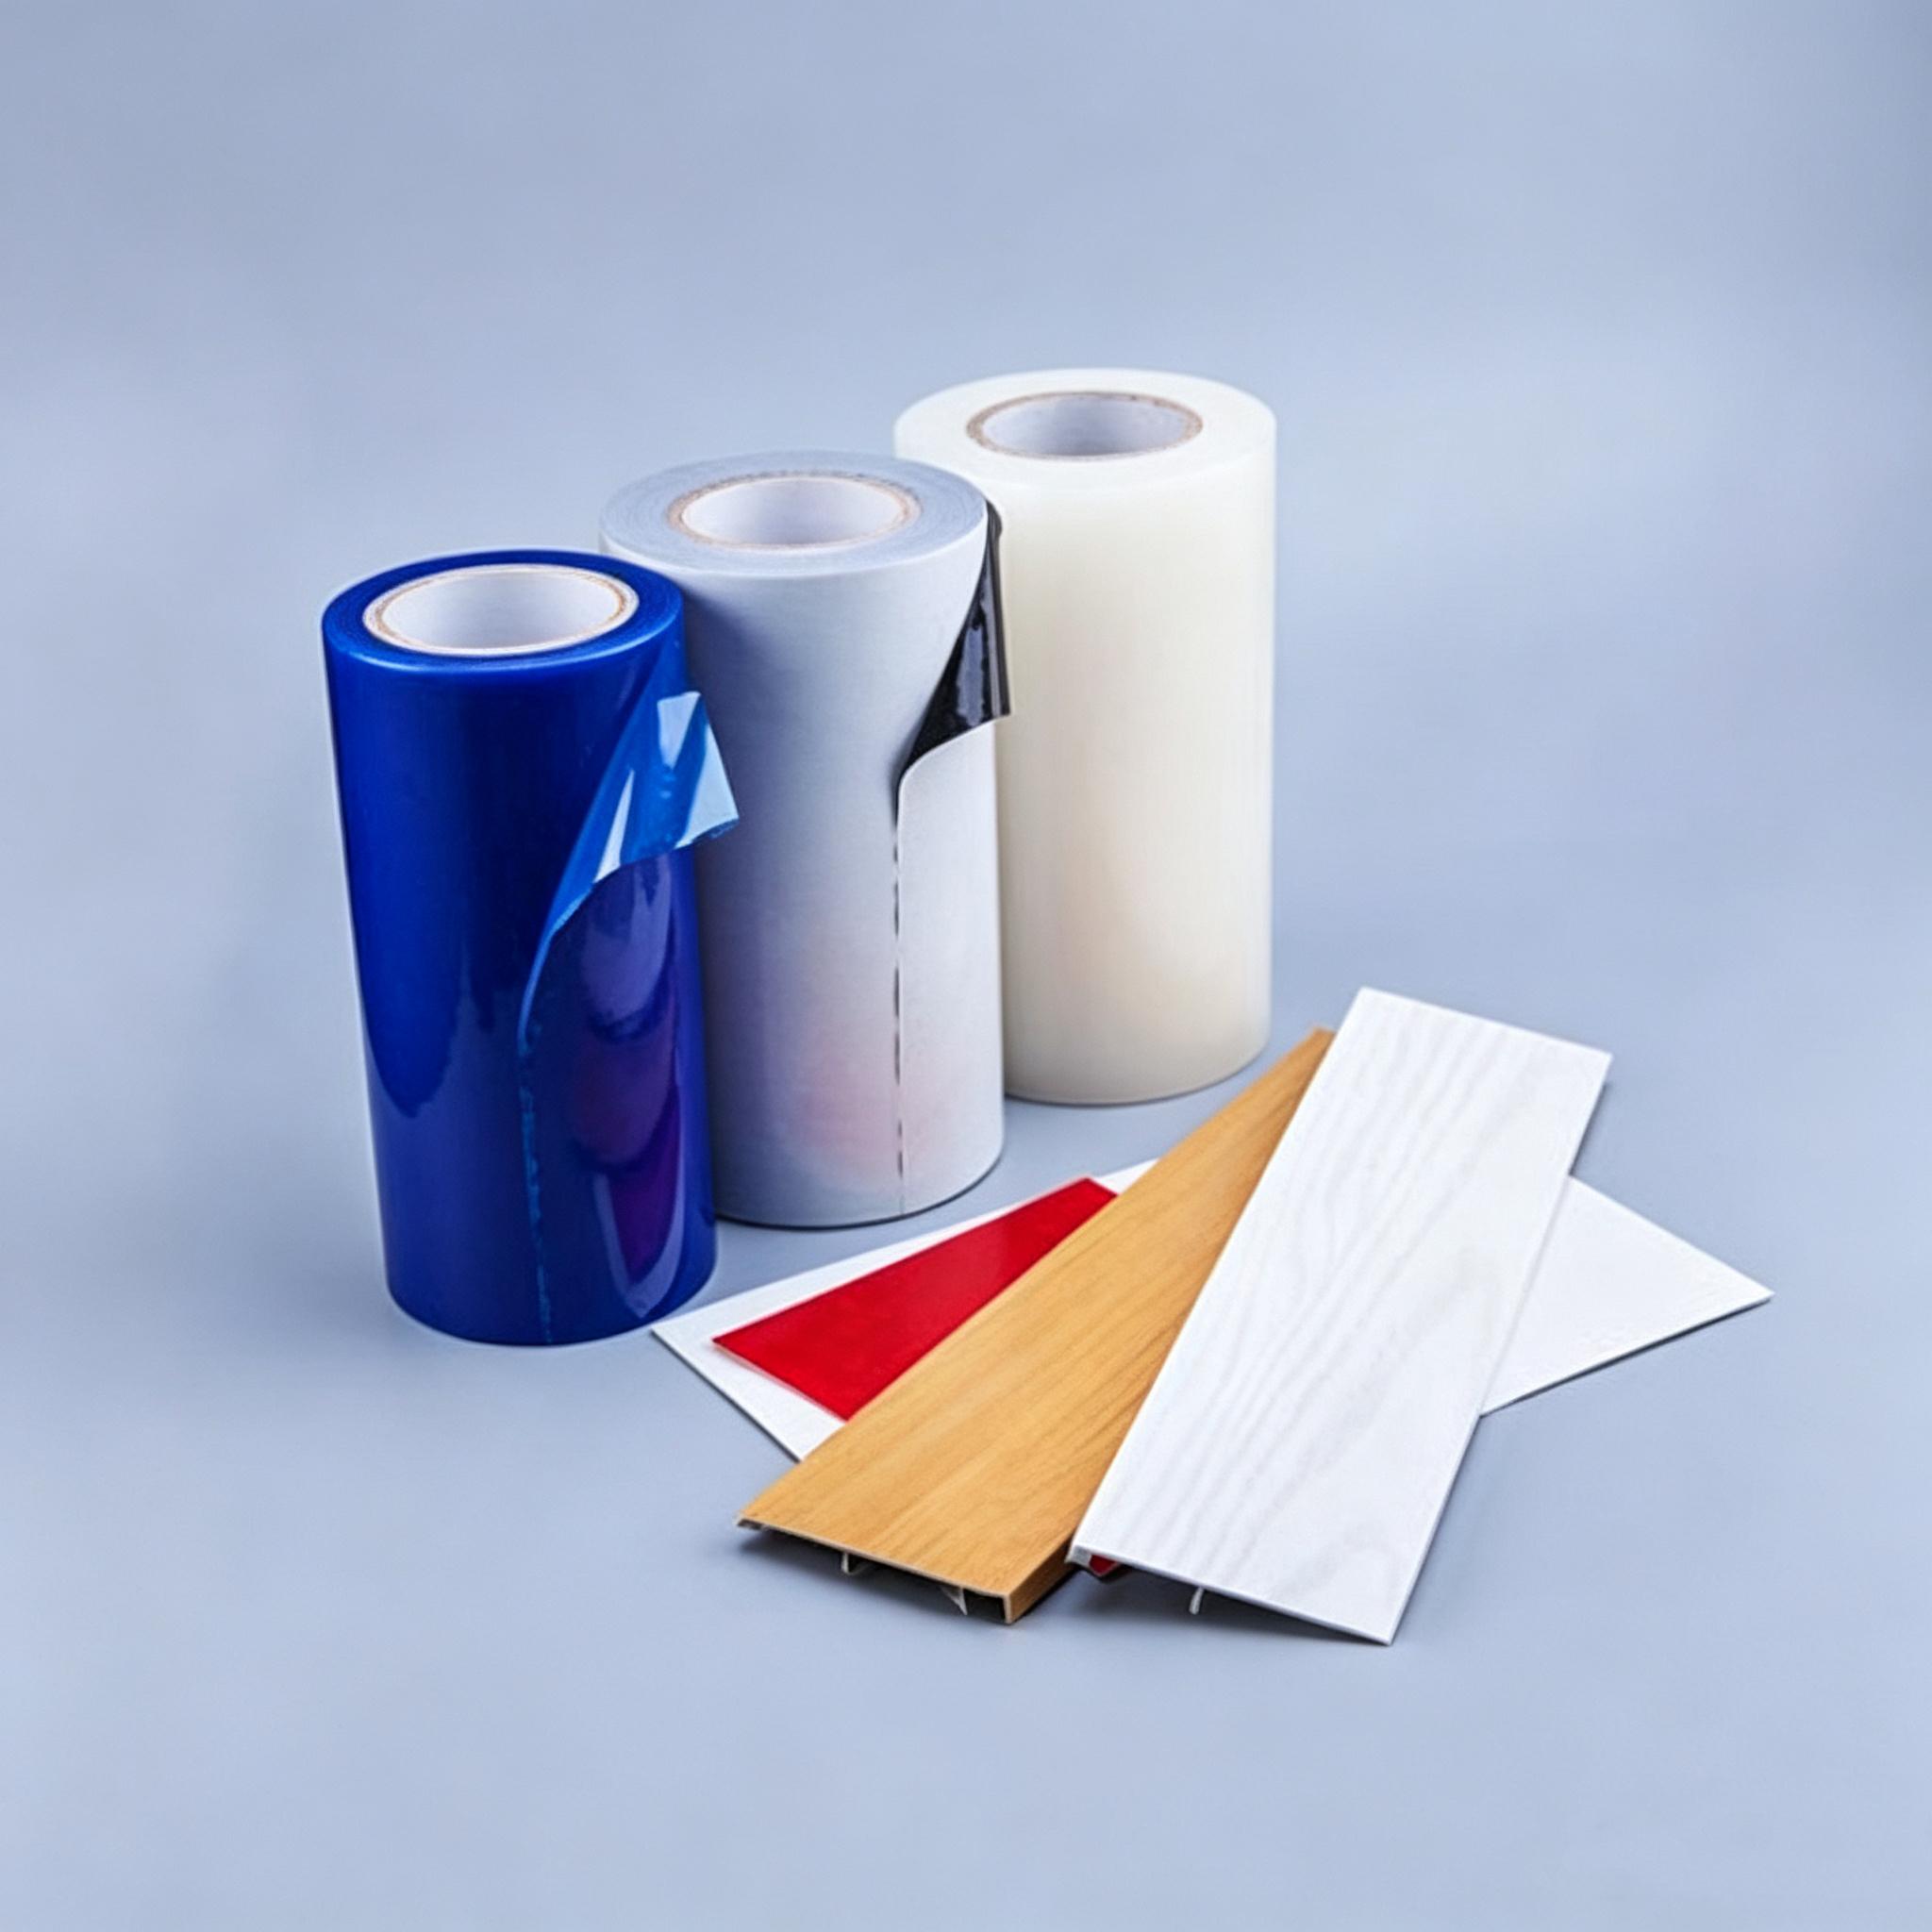
Most factory tours hand you a glossy brochure and a staged walkthrough. You end up learning more about the catering than the actual production. Push for raw, unedited footage from the line itself.
Real production line footage shows the noise, the pace, the occasional hiccup, and how workers actually handle materials. It exposes whether the machinery runs smoothly or gets propped up by temporary fixes. Polished videos hide all of that under cinematic lighting and scripted narration.
Ask suppliers to share a continuous clip from a routine shift, not a highlight reel. If they hesitate or offer only a curated montage, treat that as a signal. A factory confident in its daily operations will have nothing to hide.
Test adhesion and residue behavior on your actual surface
Don't rely on lab results alone—run a quick patch test on the actual surface you'll be covering. Different finishes like low-energy plastics, powder-coated metals, or textured paints can change how the adhesive grabs and what it leaves behind.
Apply a small sample with firm pressure, wait about 20–30 minutes, then peel it back at a slow 90-degree angle. If the adhesive releases cleanly with no ghosting or tacky film, you're likely in good shape. Any stringing, haze, or aggressive pull during removal is a sign to rethink your choice.
For residue, inspect the surface under bright light at a low angle—even nearly invisible films show up as smears. If you spot transfer, try a lower-tack option or shorten the dwell time before committing to a full installation.
Compare thickness tolerances across batches, not just spec sheets
A spec sheet may promise ±0.05 mm, but what actually arrives on your dock can tell a different story. When you compare thickness tolerances across batches, you start seeing patterns that a single data sheet never reveals: one run drifting toward the upper limit, another clustering tight around nominal, a third showing unexpected spread after a supplier change. These shifts matter more than the printed range because they affect how parts stack, fit, and perform in your assembly.
Pull tolerance data from three or more separate shipments, not just the latest one. Plot the measured thickness for each batch as a simple distribution, and look for differences in mean, spread, and outliers. A supplier whose tolerance stays within spec but swings from batch to batch may cause intermittent jamming or inconsistent press fits. Comparing across batches lets you spot that instability before it becomes a line-down event.
Use that cross-batch view to set your own internal acceptance band, often tighter than the supplier's spec. If a vendor consistently runs near the edge of their tolerance, you might adjust incoming inspection frequency or ask for a process change. Thickness tolerance is not just a number on paper; it is a fingerprint of the supplier's process control, and only multiple batches will show you the true pattern.
Check how manufacturers handle climate-specific performance claims
Manufacturers love to tout impressive performance numbers, but those figures often come from ideal lab conditions. A heat pump rated for 30°F might struggle at -10°F, and an electric vehicle's range can plummet in desert heat. Before trusting any climate-specific claim, look for third-party tests that mimic real-world temperature swings. User forums and independent reviews are goldmines here—they reveal how a product actually behaves when the thermometer dips or soars.
Ask the manufacturer directly for their testing protocols. Do they publish derating curves or capacity charts across a temperature range? A credible company will share detailed data showing exactly how performance shifts from mild to extreme climates. If they only offer a single number with no context, treat that as a red flag. Also compare similar products from different brands; sometimes a cheaper unit outperforms a premium one in specific weather conditions.
Finally, consider long-term reliability in your own climate. A product may perform well during a short test but degrade faster under constant humidity or repeated freeze-thaw cycles. Look for warranty terms that explicitly cover climate-related failures. Real-world data from owners in similar regions, not just marketing brochures, will give you the clearest picture of what to expect when seasons change.
Review after-sales response times for quality issues
Reviewing response times for quality issues starts with defining what actually counts as a response. For many customers, the clock starts the moment they send an email or submit a web form, not when a support agent eventually picks up the ticket. If a defect report sits in a queue for two days before anyone acknowledges it, the customer is already forming an opinion about reliability, regardless of how quickly the replacement part ships later. Tracking only resolved-on time misses this early friction.
A practical review should pull raw timestamps from every channel: email, phone logs, chat transcripts, and CRM entries. Compare the gap between customer contact and first human reply, then break it down by product line, severity, and region. Quality issues often get routed to engineering for root cause analysis, and that handoff can quietly add days. If one region consistently shows a four-hour delay for battery defect reports while others respond in twenty minutes, the problem is not the support team's effort; it is a routing or staffing issue that needs a specific fix.
After identifying the bottlenecks, set response targets that reflect actual customer impact rather than an arbitrary one-hour rule. A cosmetic paint flaw can wait longer than a brake system failure. Make the review findings visible to quality and production teams, because a spike in delayed responses for a particular batch number may signal an upstream manufacturing problem that support agents cannot solve alone. The point is to build a loop where slow response times trigger investigation before customers leave, not after they have already posted a negative review.
FAQ
Dig into their resin sourcing. Ask specifically which polyethylene or polyolefin grades they use, and whether they can show batch-level incoming inspection records. A manufacturer that openly shares supplier names and test data for tensile strength and elongation is usually one you can trust. Also watch for inconsistencies in film clarity or tack—cheap recycled content often shows up as slight haze or uneven adhesive transfer even before application.
Request accelerated weathering tests, like QUV or xenon arc, run for at least 300 to 500 hours. Then ask for a real-time outdoor exposure sample from the same production line, not a lab-only batch. Clean peel depends on the adhesive system, so also ask for 180-degree peel force measurements at both low and high speeds. A decent maker will provide these without hesitation.
It comes down to the adhesive chemistry and the film's surface energy. Cheaper factories often use general-purpose acrylic adhesives that are too aggressive or degrade unevenly. Better ones either formulate low-tack rubber-based adhesives or use UV-stable acrylics with controlled crosslinking. Ask the manufacturer for data on how their adhesive behaves on polycarbonate, PMMA, and coated metals after 60 days at 60°C—residue-free performance should be proven, not promised.
Look for an ISO 9001 certificate that is actually tied to film production, not just trading. More telling are process control charts for coating thickness and peel force, along with in-line defect detection records. If a factory can show SPC data for the last three months and a corrective action log with real root-cause analyses, you have found a supplier that treats QA as a daily discipline rather than a final inspection formality.
The release liner's stiffness and unwind force matter more than most buyers realize. A film that unwinds unevenly or has a liner that tears easily will jam robotic applicators. Ask the manufacturer to provide liner release values measured in grams per 25 mm at both low and high peel speeds, and request a sample roll that matches your line's maximum unwind speed. A factory that understands automation will ask about your equipment before quoting specs.
In-house coating gives you a single point of accountability and faster adjustments when tack or thickness drifts. Outsourced coaters can work, but then you are relying on the film converter to audit someone else's quality. Ask directly: 'Do you coat your own adhesive or buy coated jumbo rolls?' If the answer is vague, move on. A manufacturer with its own coating line can usually tell you the slot-die width and drying oven length, which are strong indicators of process control.
Watch the raw material storage area. If resin bags are opened, half-used, and left exposed to humidity or dust, that contamination will end up in the film. Notice whether the coating line has particle counters or just visual checks. Ask to see the reject pile—if it is suspiciously small, the factory may be reworking defective rolls and selling them as first grade. Also check if the QC lab actually has a functioning peel tester and aging chamber, not just showpieces.
Conclusion
Selecting a temporary protective film supplier in China goes far beyond comparing prices or glossy catalogues. Start by tracing the raw material sources—ask for batch-level documentation that shows resin and adhesive suppliers, not just a generic certificate. If the factory hesitates to share this, that hesitation itself is a warning. Next, request unedited video of the actual coating line in operation. You want to see real-time width, tension, and inspection steps, not a polished promotional edit. This reveals whether the plant's daily routine matches its claims. Once samples arrive, run adhesion and residue tests on the exact substrate you need to protect, including aged or slightly textured surfaces. A film that performs on glass may leave residue on powder-coated metal after UV exposure.
Beyond initial samples, compare thickness consistency across multiple batches rather than relying on a single spec sheet. A supplier that can show you statistical process control data for film gauge over several production runs is more likely to deliver uniform protection on a large scale. Pay special attention to how the manufacturer responds when you ask about climate-specific performance. If they claim high-temperature or high-humidity suitability, they should provide test data simulating your actual storage or shipping conditions—not just marketing language. Finally, evaluate their after-sales behavior before you sign. Send a simulated quality complaint and measure how quickly they respond, who takes ownership, and whether they offer a concrete corrective plan. These quiet checks often predict long-term reliability better than any factory audit.
Contact Us
Contact Person: Jack Xu
Email: [email protected]
Tel/WhatsApp: 8615257328825
Website: https://www.temporaryprotectivefilm.com/