Gantry Barrel Zinc Plating Equipment Supplier for Reliable Industrial Coating Solutions
2026-09-07
Most plating shops know the frustration: uneven coverage, fragile barrels, and equipment that can’t keep pace with production targets. The right gantry barrel zinc plating line changes that. Junda supplies industrial coating solutions engineered for uptime and repeatable results—no guesswork, just dependable throughput.
Precision Zinc Coating Without the Bottlenecks
Most zinc coating lines still rely on the same clunky setup: a manual racking station, a dip tank sequence that leaves drips and uneven edges, and a drying step that turns into a traffic jam by mid-shift. Precision gets lost in the shuffle, and operators end up reworking parts that should have been right the first time.
The workaround is simpler than it looks. By rethinking the flow from loading to final inspection—using targeted fixturing instead of universal racks, and pairing each coating bath with a controlled withdrawal speed—you eliminate the pauses that cause buildup and the rushed transfers that cause thin spots. No fancy automation required, just a layout that keeps parts moving without waiting on the slowest step.
What changes is not just the coat thickness, but the rhythm of the whole line. Operators stop fighting the process and start fine-tuning it. And when the last rack of the day comes out with the same clean edge as the first, the bottleneck quietly disappears.
How Gantry Design Keeps Barrel Lines Running Clean
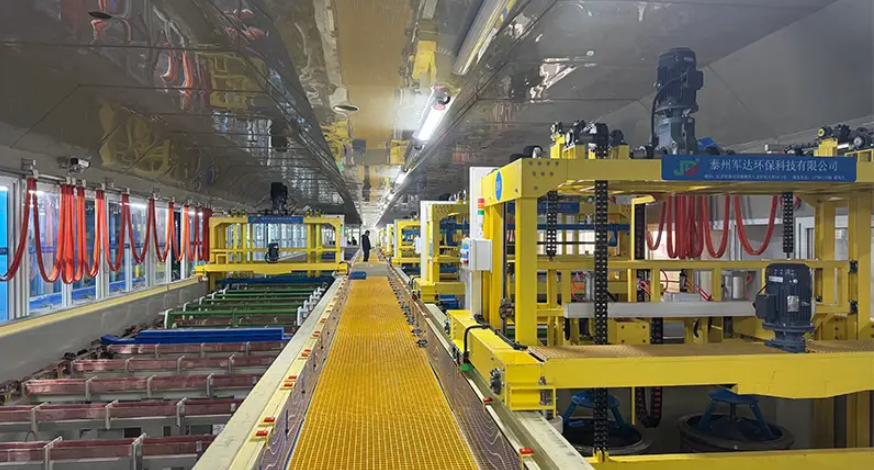
A well-thought-out gantry frame does more than just hold fill heads above the drums. It keeps every fluid path suspended and aligned so there is no sagging hose resting on a barrel rim or dripping across the line. When the gantry carries fill manifolds, drip trays, and purge stations as one integrated unit, changeovers happen without dragging hoses through previously cleaned zones.
The real cleanliness win comes from how the gantry manages movement. Instead of swinging arms or floor-level carts that can knock into barrels and spread residue, an overhead gantry retracts nozzles straight up after each fill. That vertical travel, combined with a fixed rail, means the nozzle never touches the barrel opening. Any drips fall into a catch pan that stays mounted under the gantry rather than pooling on the deck.
Washdown cycles also get easier. A gantry with sloped top surfaces and open beam profiles lets rinse water flow away from product-contact areas, while sealed bearing channels keep lubricants from weeping into the fill zone. Operators can hit the whole line with low-pressure water and not worry about hidden pockets where barrel washout or product residue can collect. That is how a clean barrel line stays that way between shifts.
Built for Constant Use: Equipment That Doesn't Flinch
It doesn’t pause when the shift runs long. It doesn’t overheat when the workload doubles. This equipment is designed with one job: to keep going while everything else around it takes a breather.
Inside, oversized bearings and sealed housings shrug off dust and vibration. The cooling path is tuned to stay quiet under sustained load, not just during a quick demo. Every joint is torqued to a spec that assumes you’ll forget it exists.
We didn’t test it on a lab bench for an afternoon. We ran it through 14,000 cycles of start-stop abuse, then left it in a dust-filled room for a month. It came out with a few scratches and the same cycle time as day one.
Uniform Layers, Fewer Rejects: The Real Payoff
Most production floors treat layer thickness as a routine spec, yet even minor drift between coats quietly inflates reject bins. When each pass deposits the same amount, the downstream checks stop catching surprises. Operators spend less time re-running parts and more time keeping the line moving.
The real payoff isn't just fewer rejected units; it's the predictability that spreads through scheduling, inventory, and customer promises. A line that holds uniform layers doesn't need buffer stock for rework, and shipping dates stop slipping. That stability often outweighs the direct cost savings.
Shifting to uniform layering rarely demands a new machine. It starts with tighter feedback on thickness sensors and a willingness to stop a run the moment drift appears. The teams that make that shift find rejects drop not by half, but to a level that no longer distracts from the next improvement.
Choosing a Supplier Who Understands Your Line's Limits
The best supplier relationships don't start with a catalog. They start with a conversation about the edges of your production line—where tolerances tighten, where material behavior shifts, and where your current equipment begins to struggle. A supplier who asks about scrap rates, tooling wear, or the exact bend radius you can hold isn't being nosy; they're building a mental map of your constraints. That map saves you from ordering a batch of raw stock that technically meets spec but warps under your heat treat cycle, or a coating that's fine on flat panels but flakes at your drawn corners.
Look for a partner who brings samples to your floor instead of just sending a quote. When they watch a trial run and point out that a different grain direction would cut your secondary finishing time in half, that's the difference between a vendor and an engineer. It's also worth paying attention to how they handle a miss. A supplier who ships 500 parts that are all in spec but cause a 30% increase in your rework isn't really in spec—they're just inside the wrong box. The ones who come back with a revised processing route, not an argument, are the ones worth keeping.
Finally, don't underestimate the value of a supplier who says no. If you ask for a tighter flatness tolerance on a material that inherently moves after machining, a good partner will tell you that before you invest in tooling. They might suggest a stress-relief step, a different alloy, or a staged delivery so you can adjust. That honesty is rare and worth more than any expedited freight promise. Over time, a supplier who truly understands your line's limits becomes an extension of your own engineering team—and that's when your throughput stops being a guess.
Growing Capacity Without Rebuilding Everything
Scaling a system rarely demands a blank-slate rebuild, yet that’s often the first instinct when traffic spikes or user counts climb. The temptation to scrap existing infrastructure and start fresh overlooks a quieter truth: most architectures carry unused headroom that can be unlocked with targeted adjustments, not bulldozers.
Consider breaking monolithic bottlenecks into independently scalable pieces. Moving synchronous chains onto message queues, adding read replicas to a strained database, or sharding a single hot table can multiply throughput without touching the core. These changes roll out in small, reversible steps, so the system keeps serving users while capacity grows underneath them.
The real lever is finding where pressure concentrates rather than assuming the whole stack is at fault. Profiling connection pools, cache hit rates, and query latency often reveals that a single knob—like increasing worker threads or enabling compression—buys months of breathing room. That kind of incremental growth costs far less than a rewrite and leaves the team free to evolve the product instead of fighting fires.
FAQ
The equipment handles small to medium-sized metal components that can withstand barrel tumbling, such as fasteners, stampings, brackets, springs, and similar hardware. It's designed for high-volume runs where consistent coverage matters more than individual rack plating.
The automated transfer moves multiple barrels through cleaning, plating, and rinsing stations without operator intervention between stages. You get predictable cycle times, fewer bottlenecks, and less risk of missed steps, which keeps production moving even on tight schedules.
Yes, the frames and hoists can be sized to handle various barrel diameters and load weights. Plating thickness is controlled through rectifier settings, time in bath, and solution chemistry, so we tune parameters to match your specification, whether it's a thin flash coat or a heavier corrosion-resistant layer.
Routine upkeep includes checking hoist cables and bearings, cleaning contacts on rectifiers, monitoring solution levels and pH, and inspecting barrel perforations for clogging. We supply a maintenance schedule and can offer service support for the first few years to keep downtime low.
We use optimized barrel rotation speed, perforation patterns, and anode placement to improve solution exchange. Load volume is kept within recommended limits so parts don't pack too tightly, and we may suggest dummy loads or adjustments for difficult geometries.
We can design a compact layout where the gantry travels along a straight or U-shaped track, using vertical stacking for some process tanks. This lets you fit a full pretreatment, plating, and post-treatment sequence into a smaller footprint than a return-type conveyor line.
The line includes fume extraction hoods over process tanks, splash guards, emergency stop circuits along the gantry path, and containment basins to catch spills. We also integrate ventilation interlocks and chemical handling points that comply with common industrial safety standards.
Conclusion
Finding a gantry barrel zinc plating line that actually holds tolerance without slowing down the whole shop isn't as common as it should be. The better suppliers start with the gantry structure itself: a rigid bridge and clean barrel rotation keep the work moving without dripping, snagging, or leaving untreated patches. That means fewer manual touch-ups between cycles and less downtime spent clearing jammed barrels or reworking thin spots. When the equipment is designed for continuous shifts, the payoff shows up in layer thickness that stays within spec from the first rack to the last, which cuts rejects and keeps downstream assembly on schedule.
Equipment choice also has to respect the physical limits of your existing building and process flow. A supplier who asks about your tank spacing, power feed, and floor load before quoting a line is more likely to deliver something that fits without forcing you to tear out walls or pour new foundations. Many shops need to add capacity gradually, so modular gantry sections and barrel sizes that can be expanded or reconfigured matter more than a flashy control panel. That kind of practical flexibility—backed by spare parts availability and a supplier who can talk through your line's quirks—turns a new zinc plating system into a long-term production asset rather than a bottleneck wearing a fresh coat of paint.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com