Steel Rule Manual Bender Factory for Die Making Explained
2026-10-19
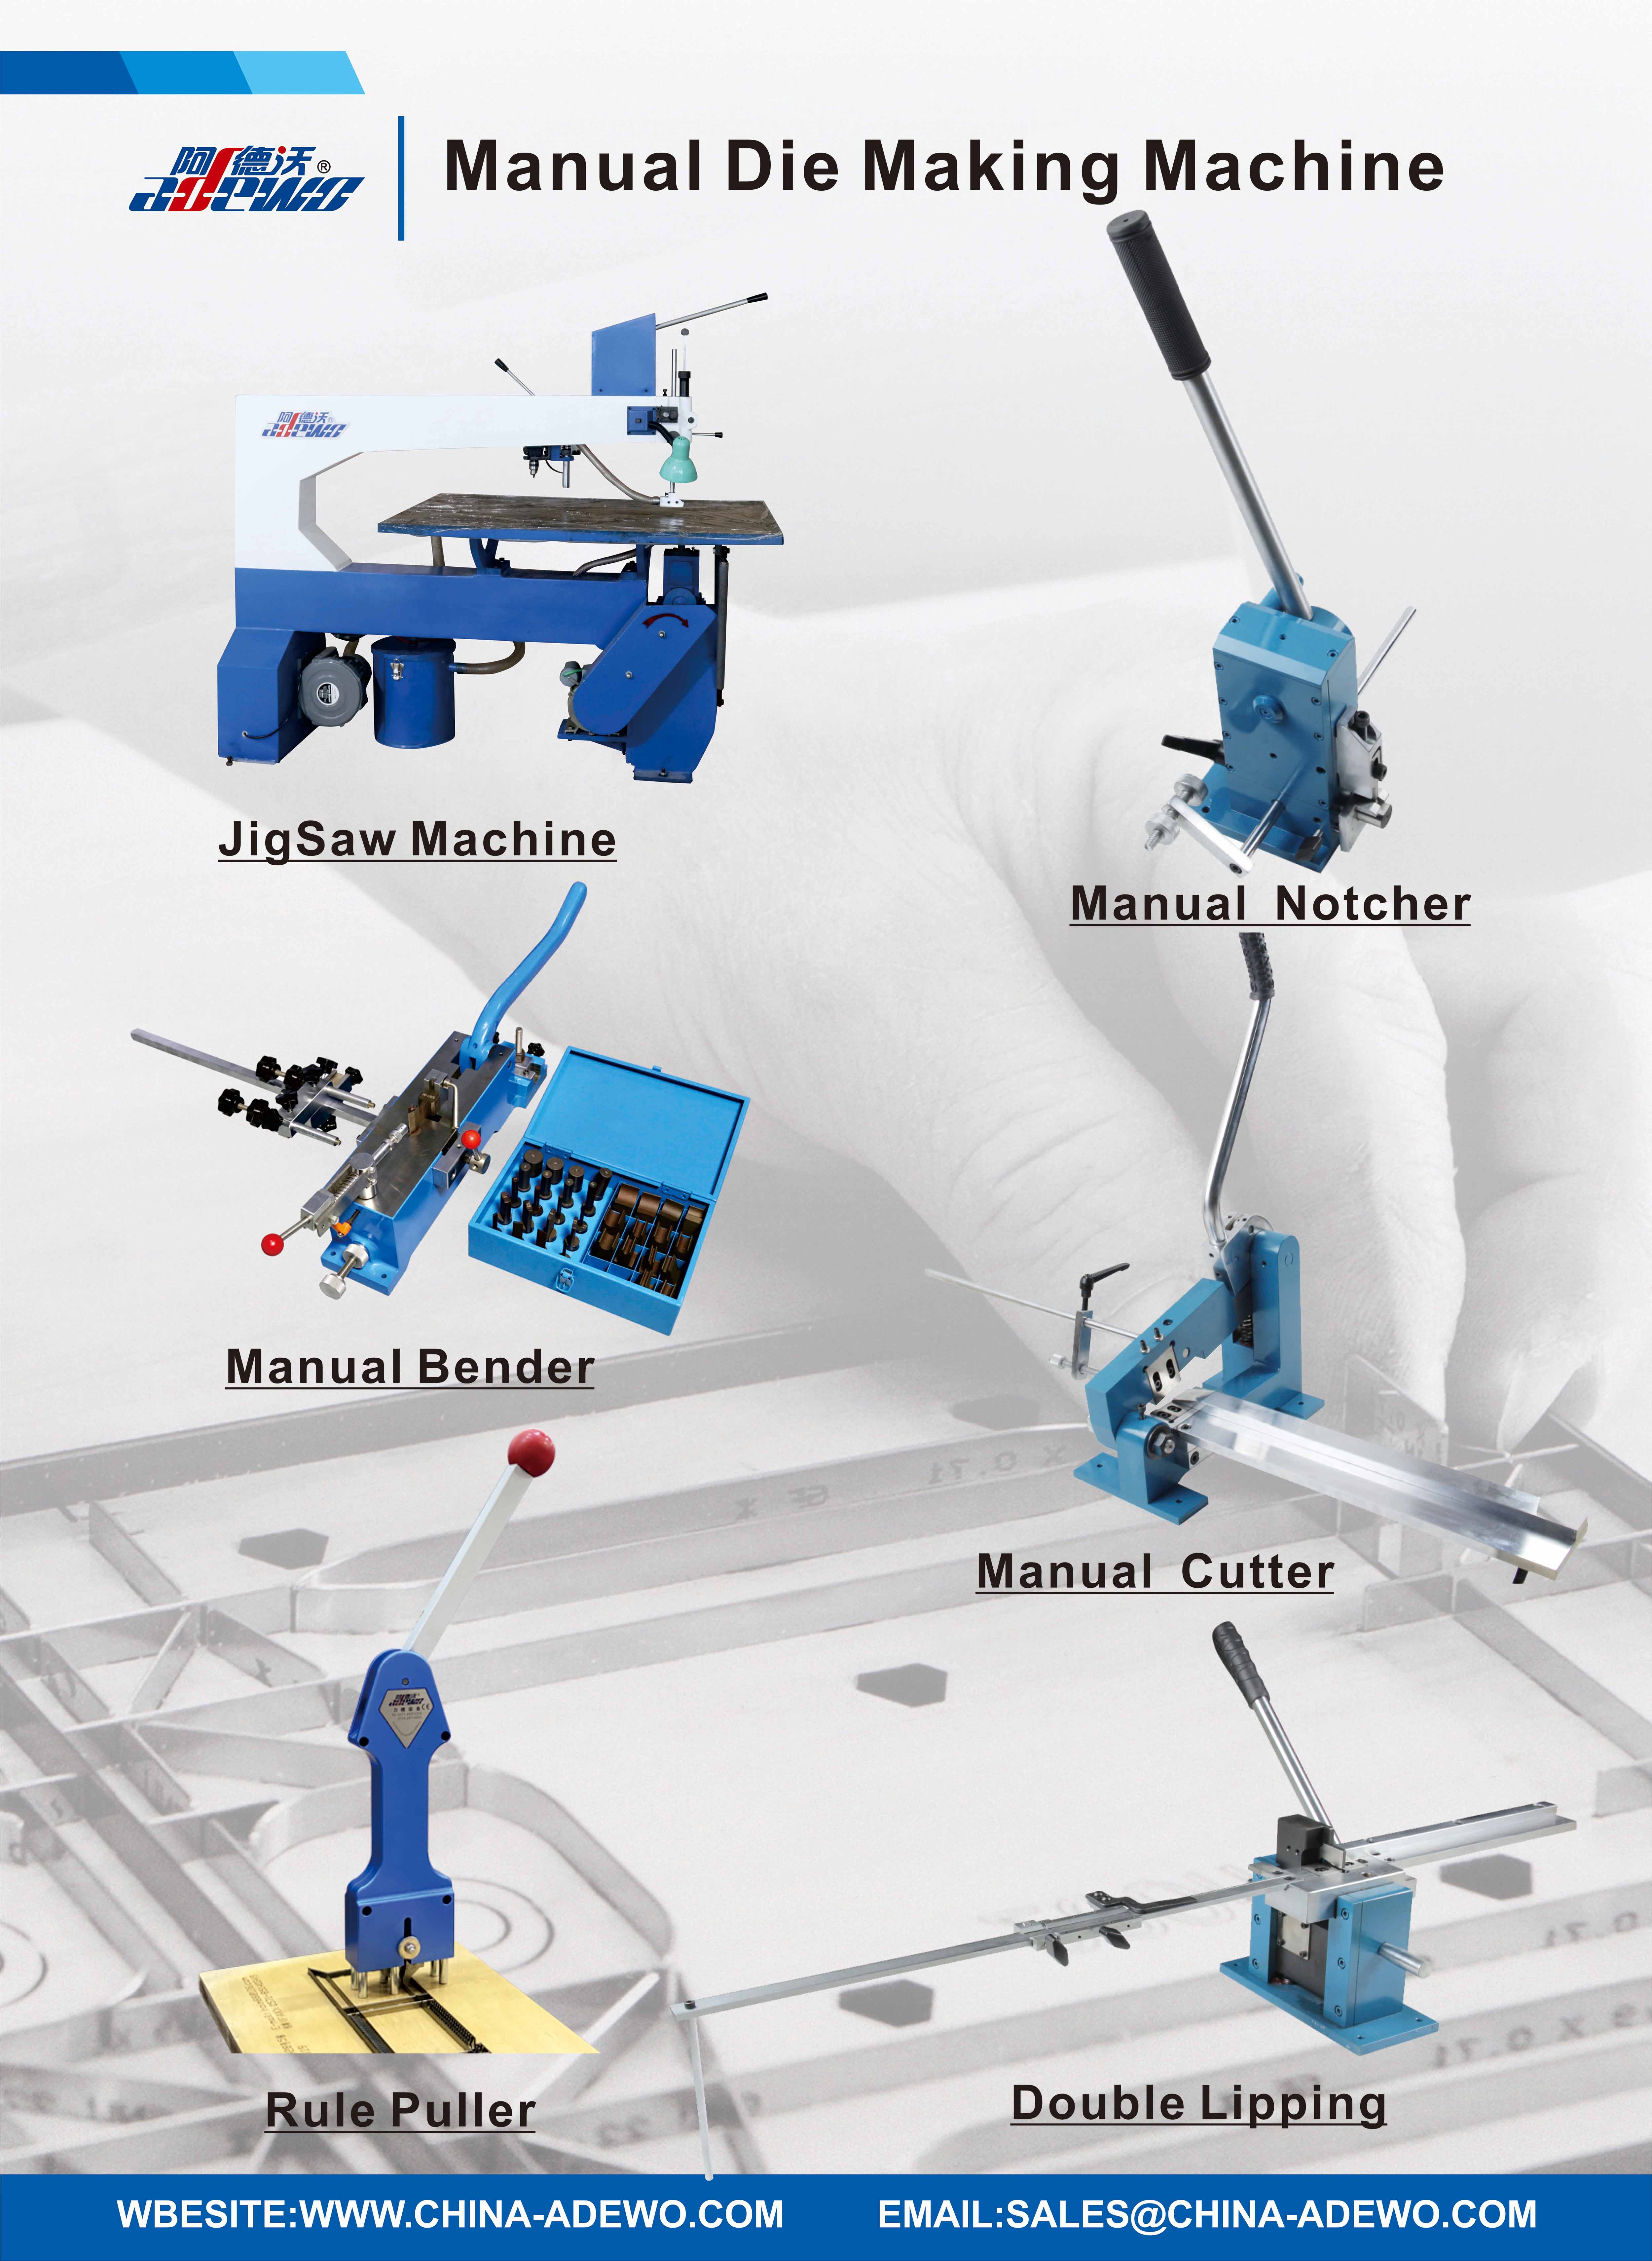
What if the weakest link in your die-making process isn't your cutting rule, but the manual bender shaping it? At ADEWO, a dedicated steel rule manual bender factory, we've seen how small mechanical differences separate crisp, repeatable bends from costly scrap. This guide explains the machinery behind steel rule bending for die making—what to look for in a factory, how manual benders actually perform, and why ADEWO's approach is built for shops that can't afford guesswork. Read on to see the details most suppliers leave unspoken.
What Happens on the Bending Floor Before a Die Takes Shape
On the bending floor, the first thing that happens is rarely the bending itself. Operators spend time checking the blank against the setup sheet, verifying grain direction and material thickness, and confirming that the backgauge fingers are set to the right positions. These small adjustments seem tedious, but they prevent most of the scrap that would otherwise show up at the die.
Next comes the test bend, usually on a scrap piece from the same lot. The angle is measured with a protractor or digital gauge, and springback is noted. If the bend comes out a degree or two off, the operator tweaks the punch depth or changes the dwell time. It is this back-and-forth that dials in the bend allowance long before any final die geometry is locked.
Only after the floor crew is satisfied with the sample do they sign off on the bend sequence. That sequence, along with the measured corrections, becomes the basis for the die design or the final tooling selection. Without this hands-on trial, a die would be little more than a guess.
Reading a Steel Rule’s Limits Without a Computer
Most machinists treat a steel rule as a trusty sidekick—quick, direct, and always within arm’s reach. But even a simple length check has hidden limits. The first one is your eyes. Under shop lighting, the gap between the 1/32-inch marks starts to blur, and parallax can easily add or subtract a few thousandths. Before you trust that reading, ask whether the edge of the rule is truly flat on the part, or if a burr or chamfer is tilting it just enough to shift the line.
Another quiet source of error is the rule’s own calibration. Off-the-shelf steel rules are often stamped or etched with tolerances that can wander by ±0.005 inches over six inches—fine for rough layout, hopeless for press-fit checks. Temperature matters too, but less than most people think: a 6-inch steel rule grows about 0.0006 inches per 10°F, usually a rounding error unless you’re working in a furnace. The real killer is cumulative contact: every time the rule is slid across a rough casting or tapped against a vise, its edges wear ever so slightly, moving the zero point.
Experienced hands learn to read between the lines. They check the rule against a known gauge block at the start of a shift, ignore the first and last half-inch of the scale, and use the narrow edge—not the flat face—for scribing lines close to a shoulder. If a measurement truly matters, they reach for a micrometer. But knowing exactly when a steel rule has hit its ceiling is what separates a careful worker from a confident guesser.
Hand Pressure, Bend Angles, and the Feel of Springback
Bending sheet metal isn't just a matter of hitting a number on the controller. The way your hands feed pressure into the material changes how much angle you actually get. A slow, steady push near the die often leaves a softer transition than a quick, firm stroke across the full length.
Springback behaves like the metal is pushing back against every degree you force into it. Thinner gauges and tighter radii tend to snap back more, so many operators learn to overbend by feel rather than relying solely on a digital readout. That difference between the commanded angle and the one your fingers sense when the part relaxes is where practice turns into skill.
Small changes in hand position—closer to the clamp, farther from the bend line, or uneven across the width—can create bows and twists that no angle correction will fully erase. Reading that feedback through the handles or the manual brake gives you a truer picture of the material than any single measurement taken after the fact.
Why Some Shops Still Reach for a Manual Bender
There is a reason the manual bender still hangs on the wall next to the CNC machines. It handles short runs and one-off repairs without the setup time or programming overhead. A skilled operator can load a tube, eyeball the angle, and pull a clean bend in less time than it takes to boot up the software on a fully automated cell.
These tools also shine when space is tight or the job is odd. A manual bender can be rolled to a job site, clamped to a bench, or used in a corner where a large hydraulic unit will never fit. Shops keep them around because they are predictable, cheap to maintain, and don't care about power outages or outdated control cards.
There is also the feel factor. Manual bending gives immediate feedback through the handle—resistance, springback, and wall collapse can be sensed and corrected on the fly. That kind of control is hard to replicate with a touchscreen, and for many old-school fabricators, it remains the fastest way to get a good part out the door.
Common Mistakes That Show Up in the First Test Cut
Many editors rush through a first assembly by cramming in every shot they logged, convinced that more coverage means more options later. The result is a cut that feels like a rough data dump rather than a story. A frequent culprit is letting scenes breathe too long at the top—holding on establishing shots or reaction beats well past their welcome, which drains momentum before the scene really starts. Another sneaky issue is ignoring audio continuity: dialogue recorded on different days will have wildly different room tones, and if you don't smooth those transitions early, every cut feels like a jump in reality, even when the picture itself flows.
Beyond pacing and sound, the most damaging mistakes hide in the edit points themselves. Cutting mid-gesture or leaving a half-second of dead air before a reply can shatter the rhythm of a conversation, making performances feel stilted or amateurish. Some editors fall in love with a temp track and cut strictly to that beat, only to find that when the score is replaced or removed, the sequence collapses because the visual timing never stood on its own. The first test cut is where these issues surface—slow scenes, awkward transitions, and moments that overstay their welcome—and fixing them there saves endless pain down the line.
Keeping a Manual Bender Accurate After Years of Use
Over time, a manual bender can drift out of true even if it hasn't seen heavy daily use. The usual culprits are mundane: metal dust packed into the guide slots, dry pivot pins, or a dial that's been knocked a hair off zero. Before adjusting any stops, sweep the bend dies and rollers clean and add a light film of oil to the sliding surfaces. Then make a test bend in scrap and check it against a known angle gauge—often that alone brings the machine back to where it was.
Worn tooling is the next thing to inspect. If the groove in the bend die has widened or the follow roller shows flat spots, you'll struggle to hit repeatable angles no matter how carefully you set the stop. Keep a cheap set of calipers or a micrometer nearby and measure the critical surfaces every few months. When you're not using the bender, store it with the pressure released and the dies coated in a thin rust preventive; letting it sit under tension or in a damp corner accelerates the small deformations that ruin accuracy.
Finally, check the frame and pivot points for play. Lifting the handle with too much force—especially with an extension pipe—can bow a pin or egg out a bushing, and once that happens the bend angle changes with every stroke. Set the bender on a level surface, snug up any loose fasteners, and replace worn pivot bushings before they wallow the holes. These small habits won't make the tool look new, but they'll keep it bending the same angle on the tenth pull as it did on the first.
FAQ
It lets you shape the steel rule into the exact profiles needed for cutting dies—think creasing, scoring, and kiss-cutting forms. Instead of relying on preset programs, the operator controls every bend by hand, which is useful for short runs and custom shapes.
Cost is the obvious reason, but manual benders also allow for quick tweaks during setup. When you are working on one-off dies or repairing an existing rule, stopping to program a machine can slow things down more than a skilled operator with a hand wheel.
Most are built for standard steel rule stock—typically 0.028 inch to 0.056 inch thick, with heights from about 0.5 inch to 2 inches. Some factories also use them for stainless rule, though that requires more force and attention to tool wear.
With a good protractor and an experienced hand, you can hit within half a degree on common angles. The real challenge is repeatability across many pieces; manual work shines for small batches where each bend can be checked immediately.
Check the frame rigidity, the quality of the bending nose, and how easily you can swap tooling for different rule heights. Also look for a stop system that lets you repeat angles without re-measuring every time—simple mechanical stops save a lot of frustration.
Worn or mismatched tooling creates kinks and weak points in the rule, which leads to cracking during die use. Keeping the bending nose clean and lightly lubricated, and replacing it when grooves appear, keeps the steel from work-hardening too fast.
Yes, if the operator works in stages and uses layout marks. The process is slower than automated bending, but for intricate shapes with tight radii or unusual angles, a manual setup often gives more control over springback and final fit.
Conclusion
On the bending floor, a die starts long before any CAD file gets converted into cutting paths. The operator lays a length of steel rule against a simple fixture and begins feeling for the point where the metal stops behaving like a straight strip and starts remembering a curve. There is no monitor giving a go/no-go signal; instead the bend is checked by eye, by a quick pass of a protractor, and by the same hands that will later crease the rule into a cutting edge. Experience fills the gap that software leaves open, especially when a rule's temper varies from batch to batch or when a tight radius sits close to a pre-existing notch. Hand pressure becomes a measurement in itself—too little and the springback leaves the angle shallow, too much and the rule kinks or fractures along the inner face. Each pull on the bender's lever is a conversation with the steel, and the answer comes as a slight give or a stubborn refusal to hold a crisp corner.
Many shops keep a manual bender near the workbench not out of nostalgia but because it handles short runs, odd profiles, and quick repairs faster than setting up a CNC bending cell. That speed, however, demands discipline. A first test cut often exposes a bend that looked fine in the air but drifts when the rule is locked into a die board—common faults include a radius that is a degree open, a flange height that is off by half a millimeter, or a bend placed a touch too far from a bridge. Corrections happen at the bender, not in the cutting file. To stay accurate after years of use, the bender itself needs regular attention: pivot pins are checked for play, the bending nose is dressed smooth, and reference stops are re-zeroed against a known sample. Without that upkeep, even a skilled pair of hands starts fighting the tool instead of listening to the steel.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com